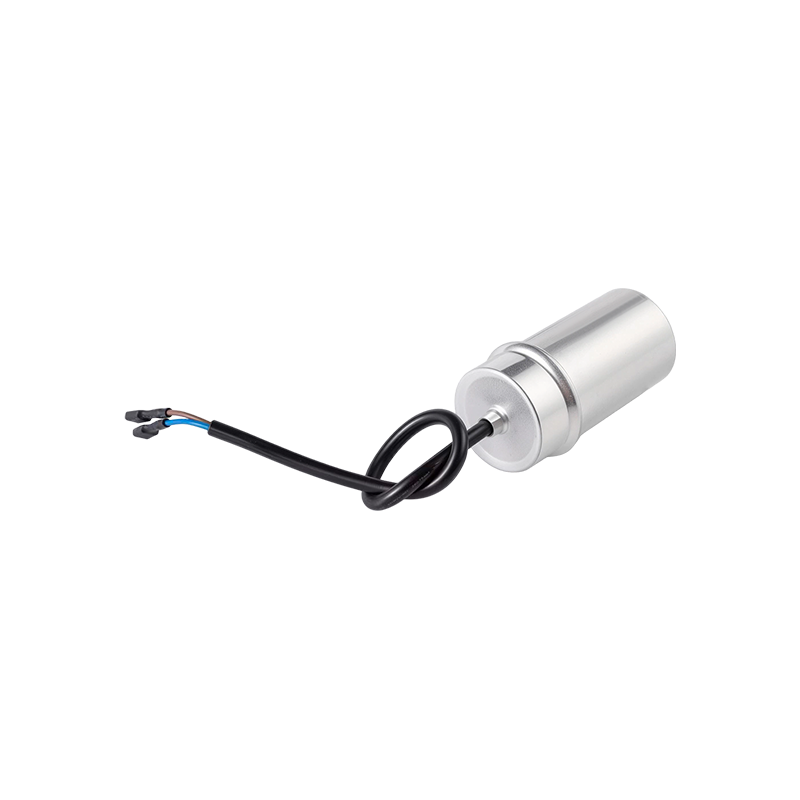
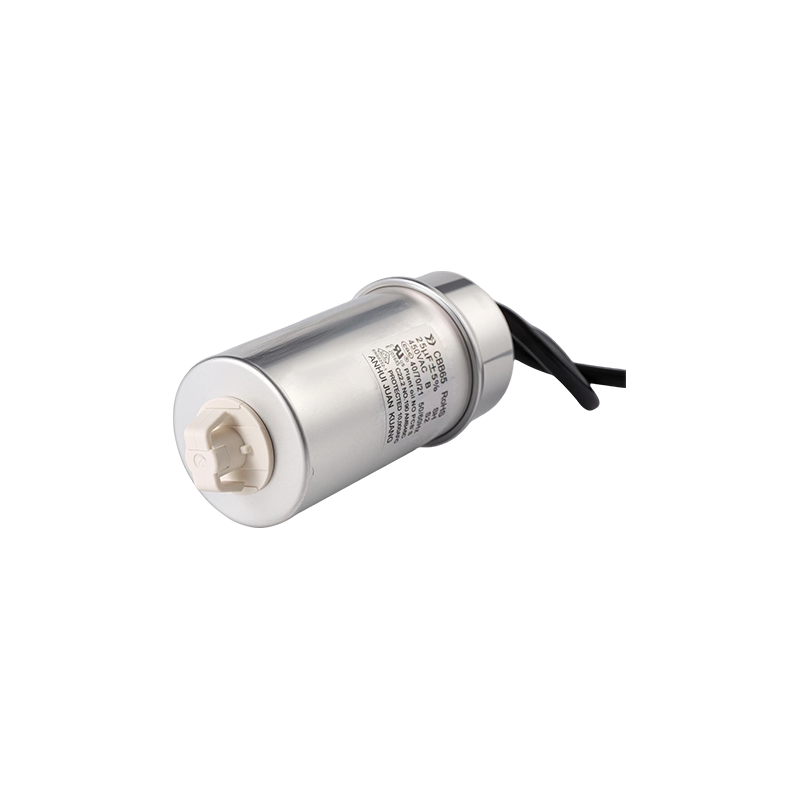
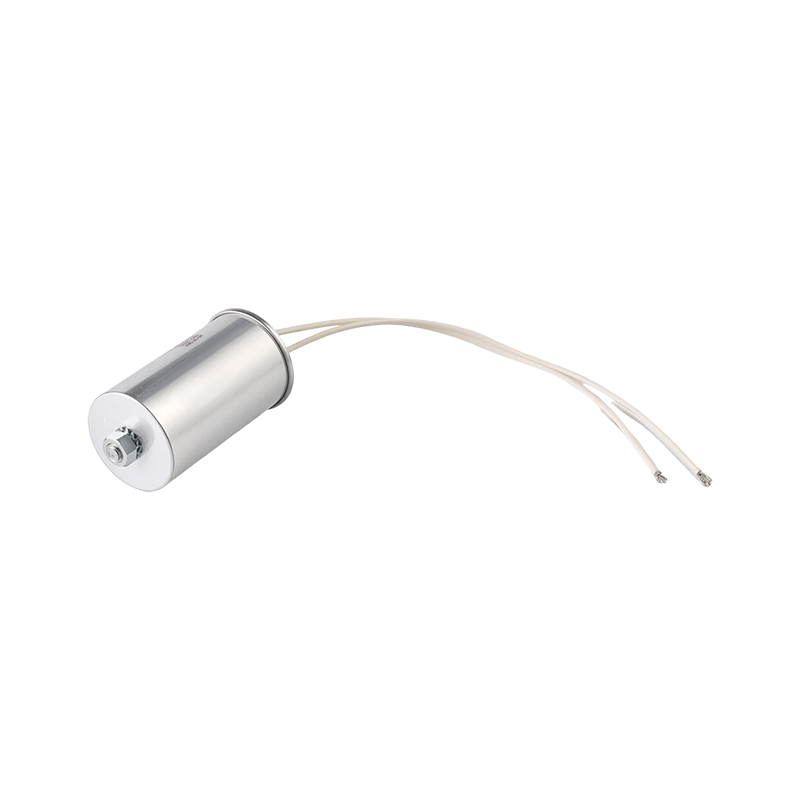
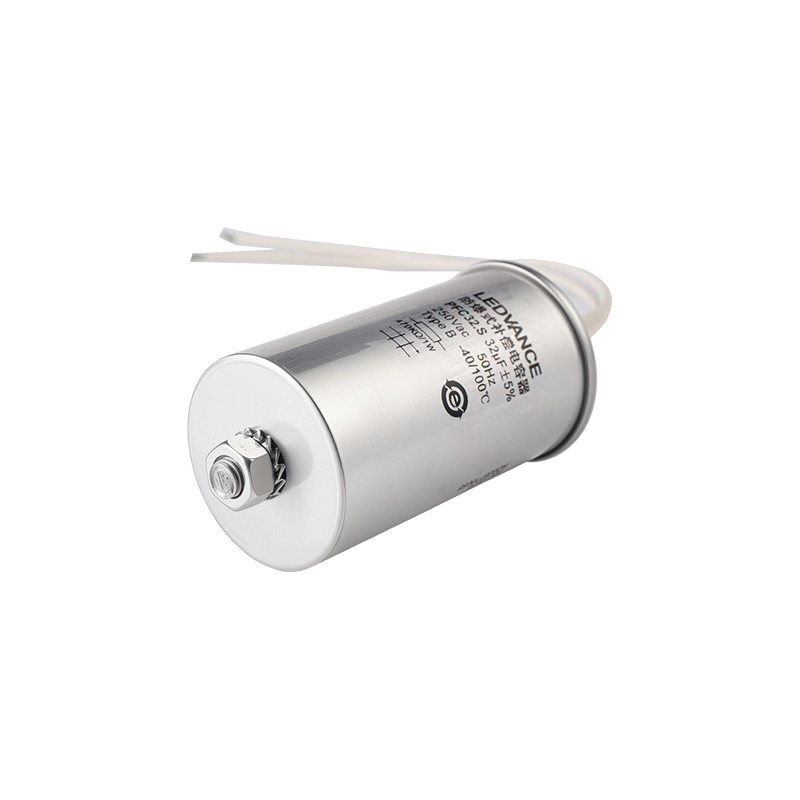
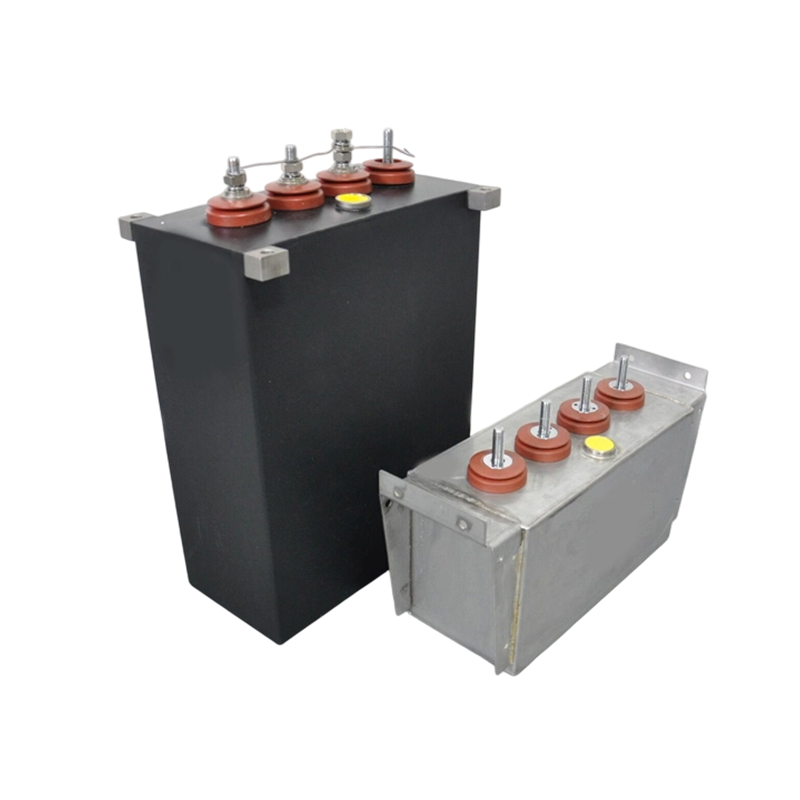
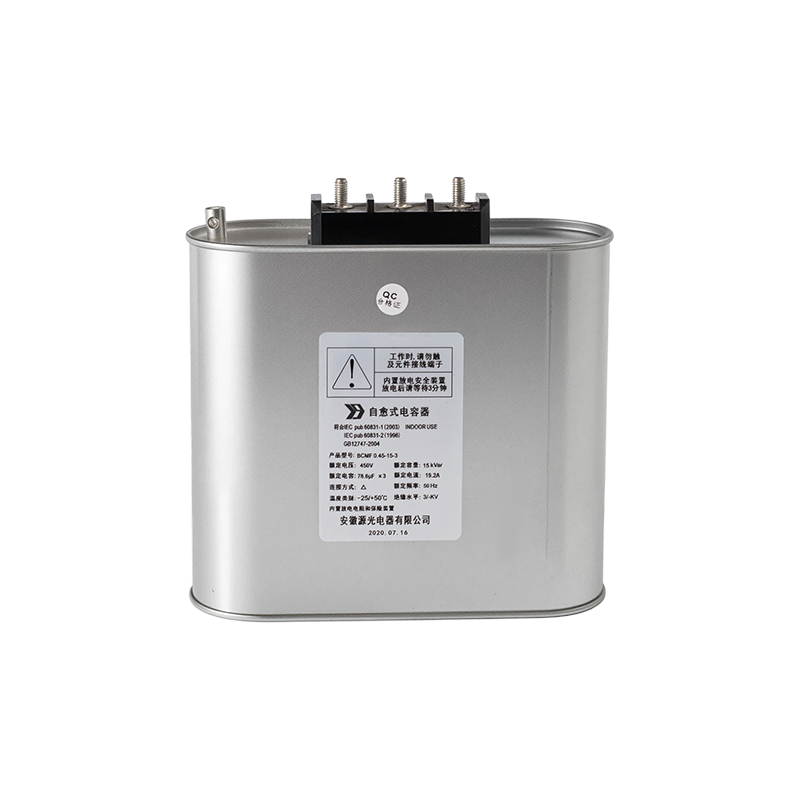
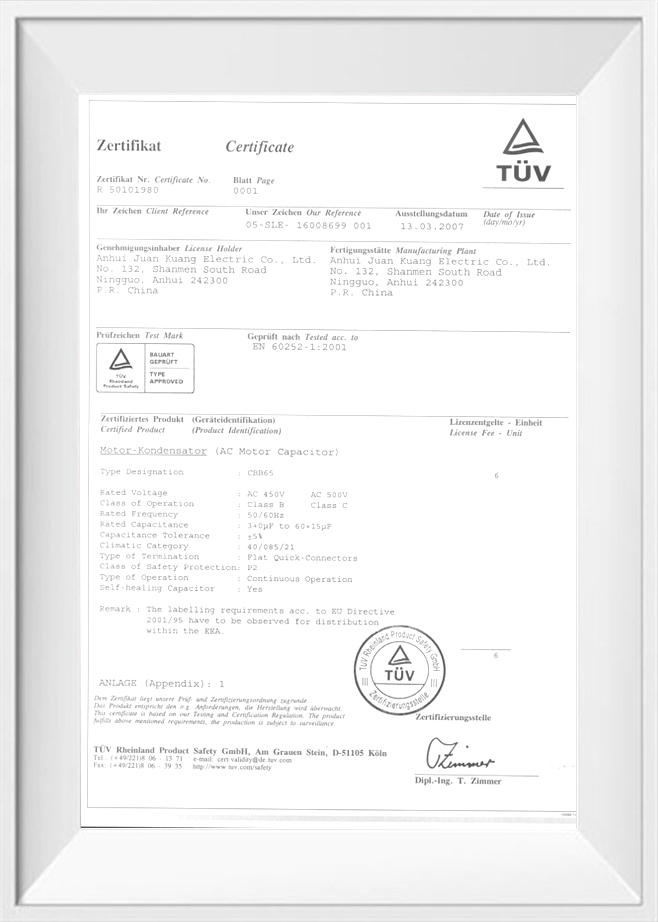
◆ Product Advantages
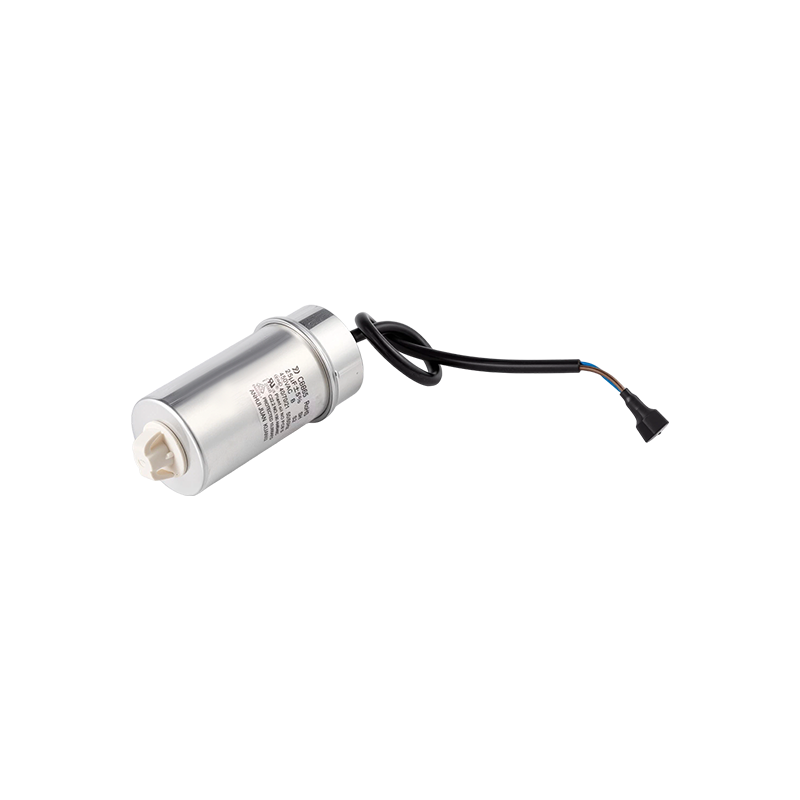
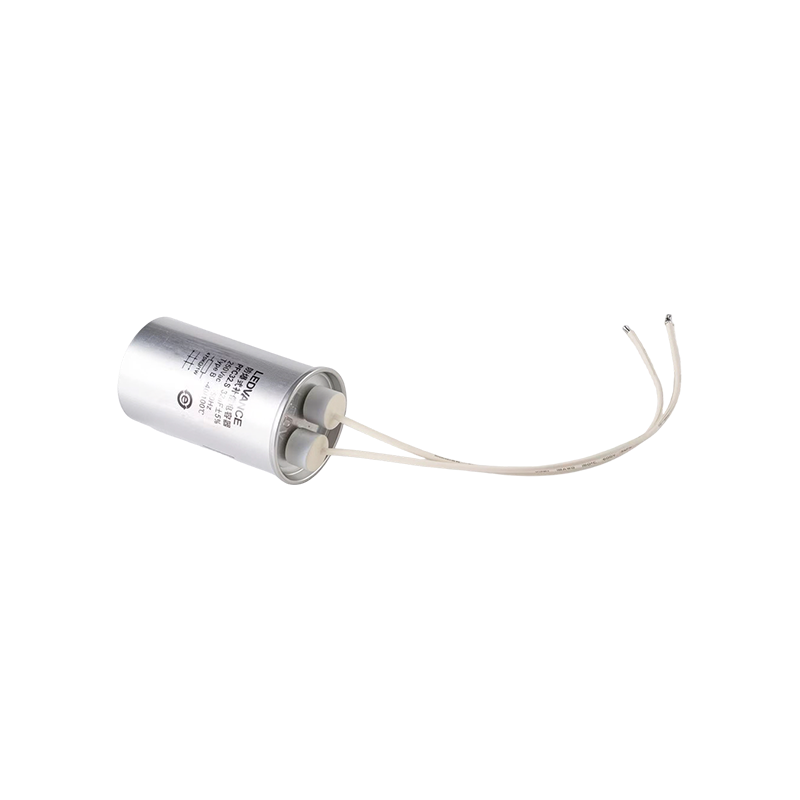
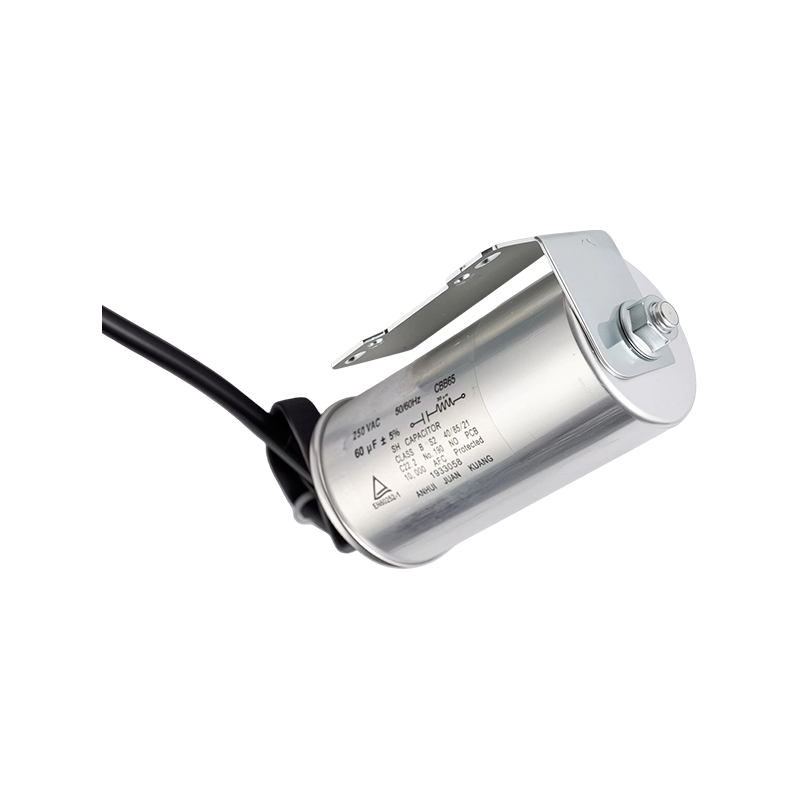
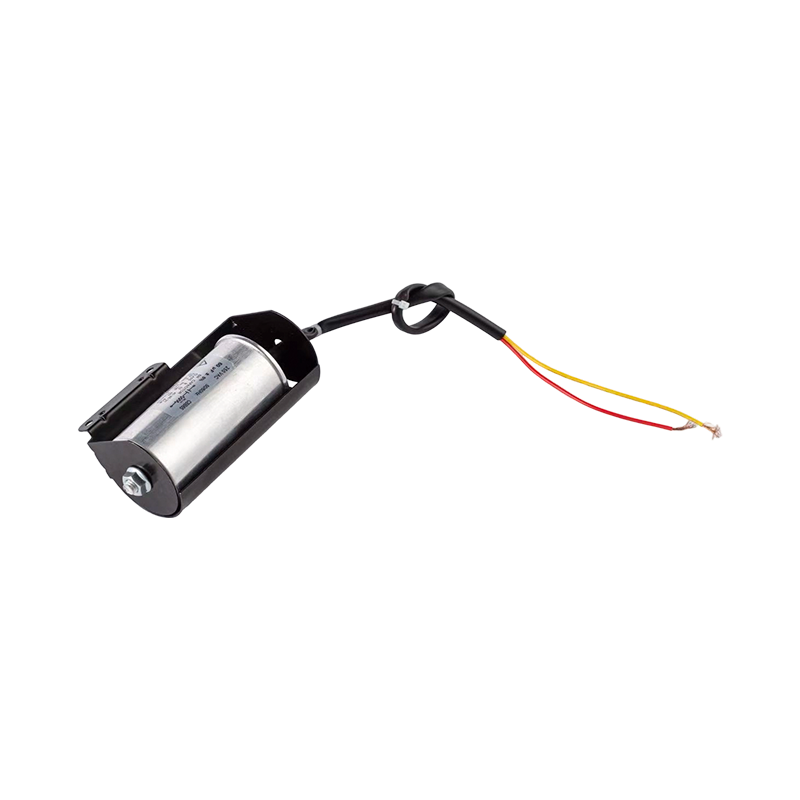
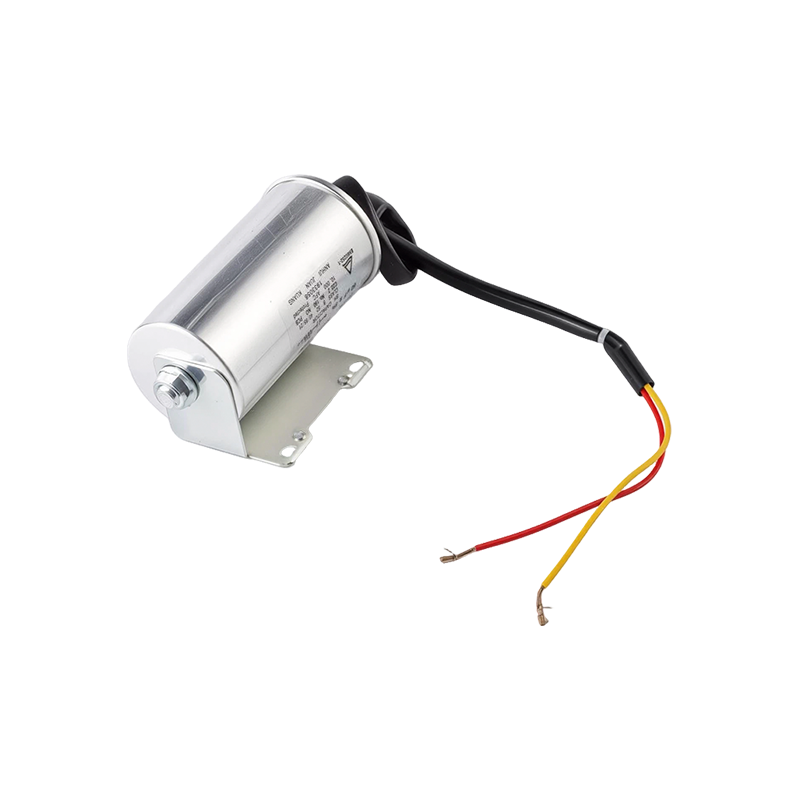
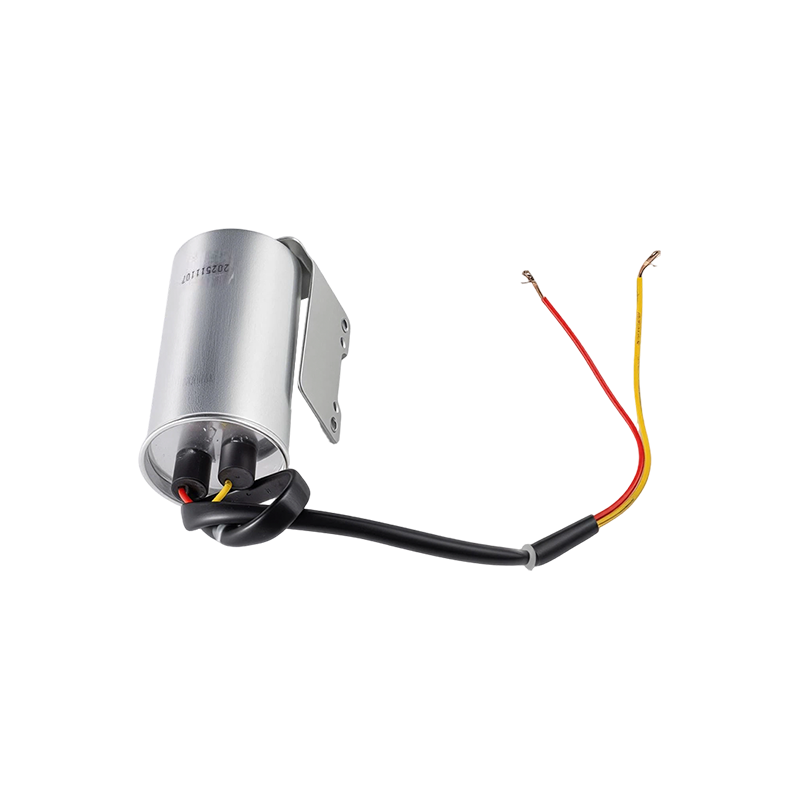
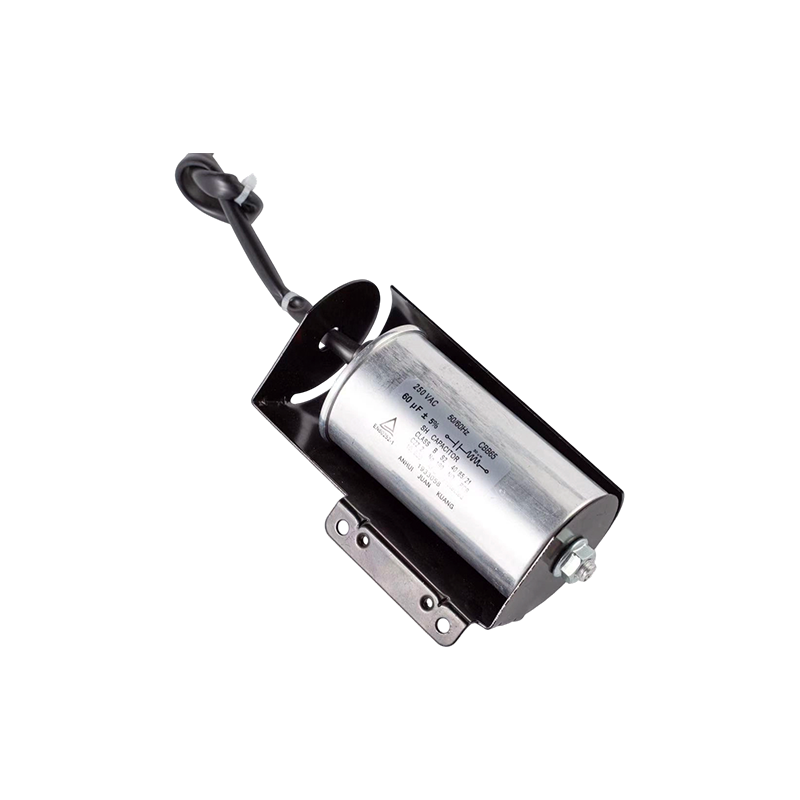
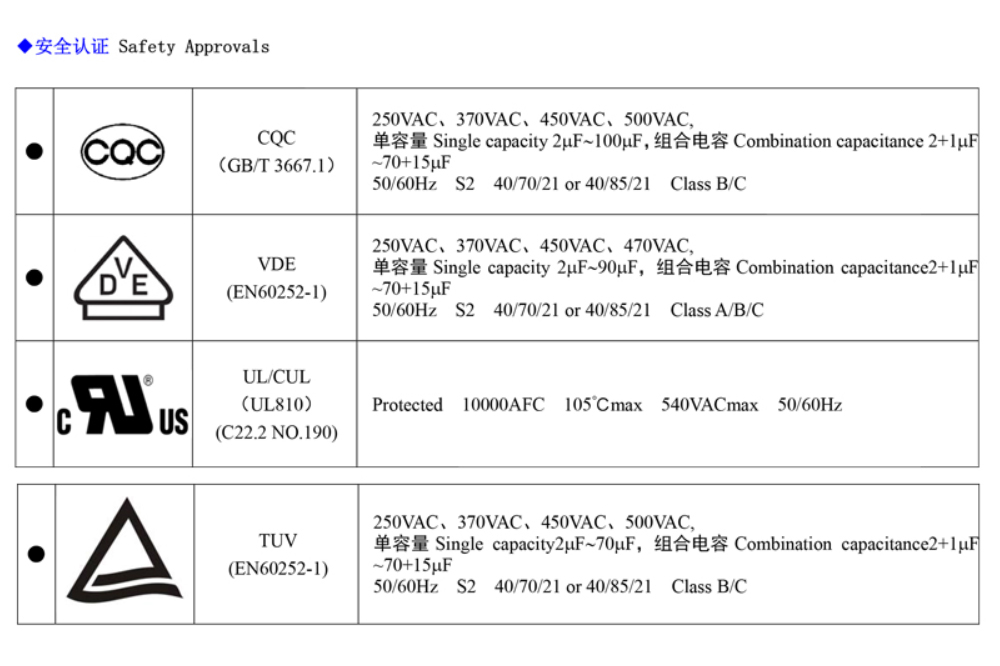
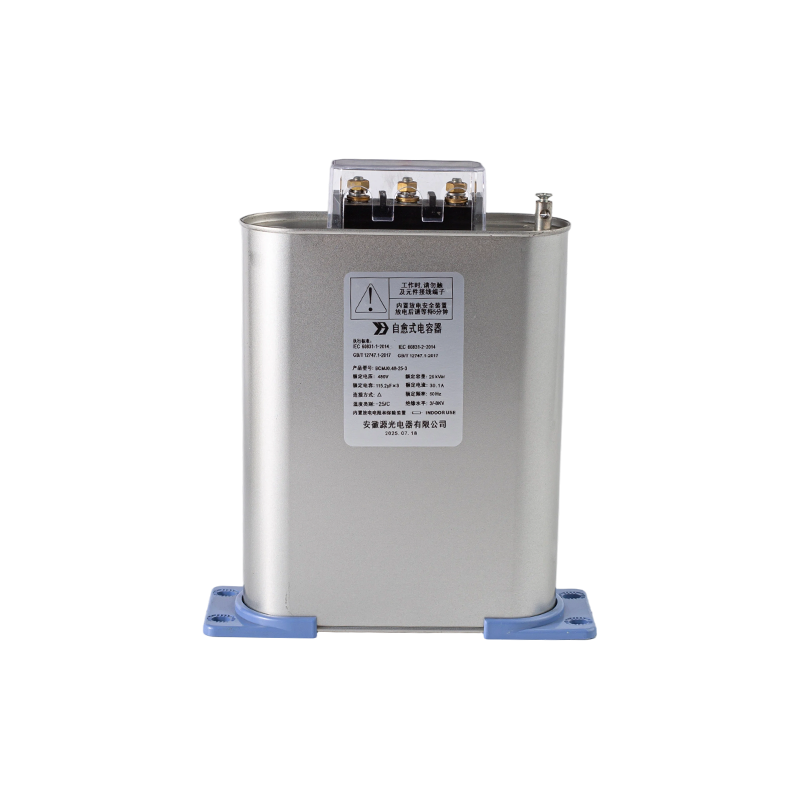
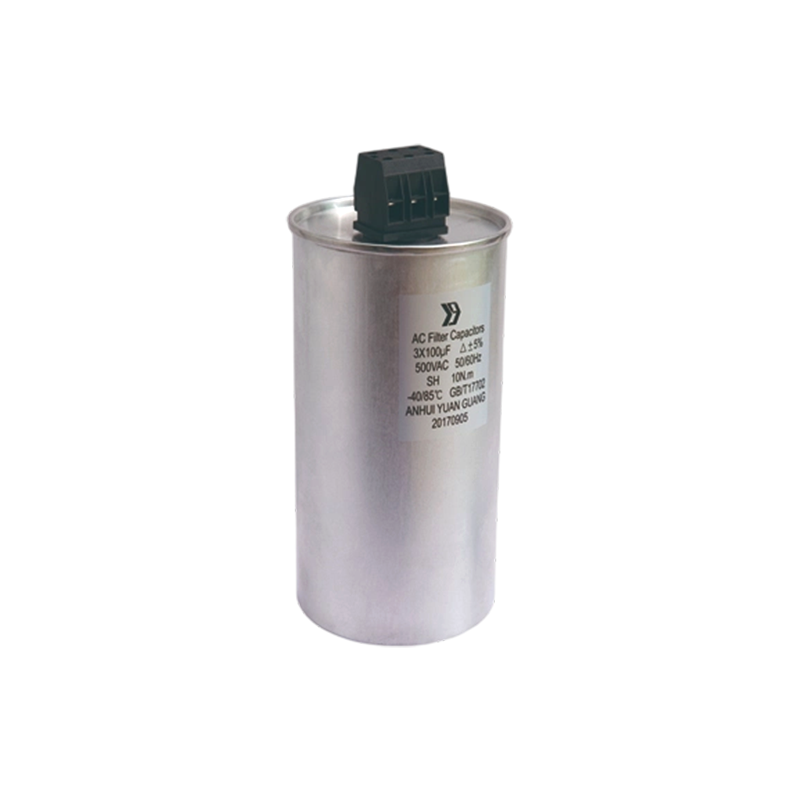
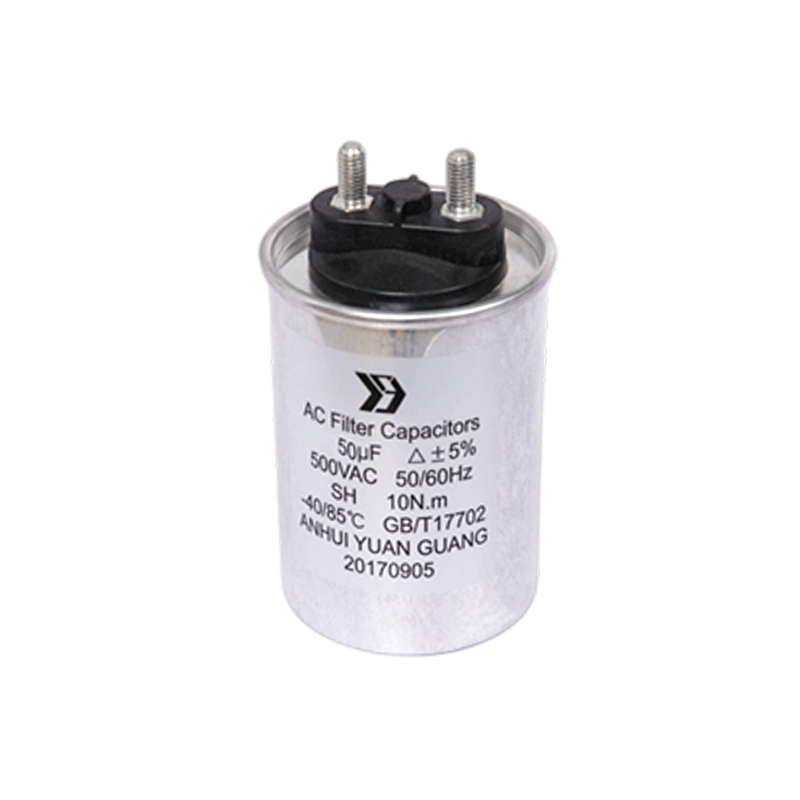
- Aluminum Case Built-In Mechanical Anti-Explosion Fully Sealed (S2 Safety Level) — Industry-Leading Safety Specification: CBB65 refrigerator aluminum case capacitors use a built-in mechanical explosion-proof fully sealed aluminum case structure (S2 safety level), with safety level significantly higher than same-specification plastic case products; the built-in mechanical pressure relief valve actively actuates upon abnormal capacitor over-pressure, completely isolating the impact of internal failure on the refrigerator cabinet, eliminating explosion and flying debris risks, and providing the highest level of active safety protection for the refrigerator unit and users
- Excellent Aluminum Case Heat Dissipation Ensuring 24-Hour Continuous Operation Stability: The thermal conductivity of aluminum alloy housing far exceeds plastic materials, efficiently transferring heat generated during capacitor operation to the housing surface for dissipation; under the round-the-clock uninterrupted refrigerator compressor operation conditions, effectively maintaining a lower internal operating temperature of the capacitor, fundamentally extending service life and reducing the risk of electrical performance degradation caused by high temperatures
- High Insulation Resistance with Long-Term Stable and Consistent Electrical Parameters: High product insulation resistance with extremely minimal fluctuation in electrical parameters (capacitance, tanδ) throughout the designed service life, ensuring consistently stable operating characteristics of refrigerator compressor motors under various ambient temperatures and loads, without refrigeration anomalies caused by capacitor performance fluctuations
- Good Self-Healing Performance with High Reliability: Metallized polypropylene film self-healing characteristic rapidly self-repairs upon localized dielectric breakdown, effectively suppressing further defect propagation, greatly reducing early failure probability, suitable for refrigerator compressor overall design life requirements exceeding 10 years
- Aluminum Case Fully Sealed for Strong Corrosion Resistance and Environmental Adaptability: Aluminum case fully sealed structure provides excellent protection against moisture, salt spray, oil contamination, refrigerant vapor, and other harmful external environmental factors, particularly suitable for long-term reliable use
 English